Explosives Industry
The low-shear, virtually pulsation-free action of a progressive cavity pump makes it well suited to conveying emulsion and gel explosives: the rotor-stator design conveys product through sealed cavities rather than high-velocity impellers.
SafetyHazardous Environment Duty
FlowVirtually Pulsation-Free
ProductProtects Emulsion Integrity
MeteringConsistent Formulation
Under Pressure Explosives Sector
A Product That Must Not Be Agitated
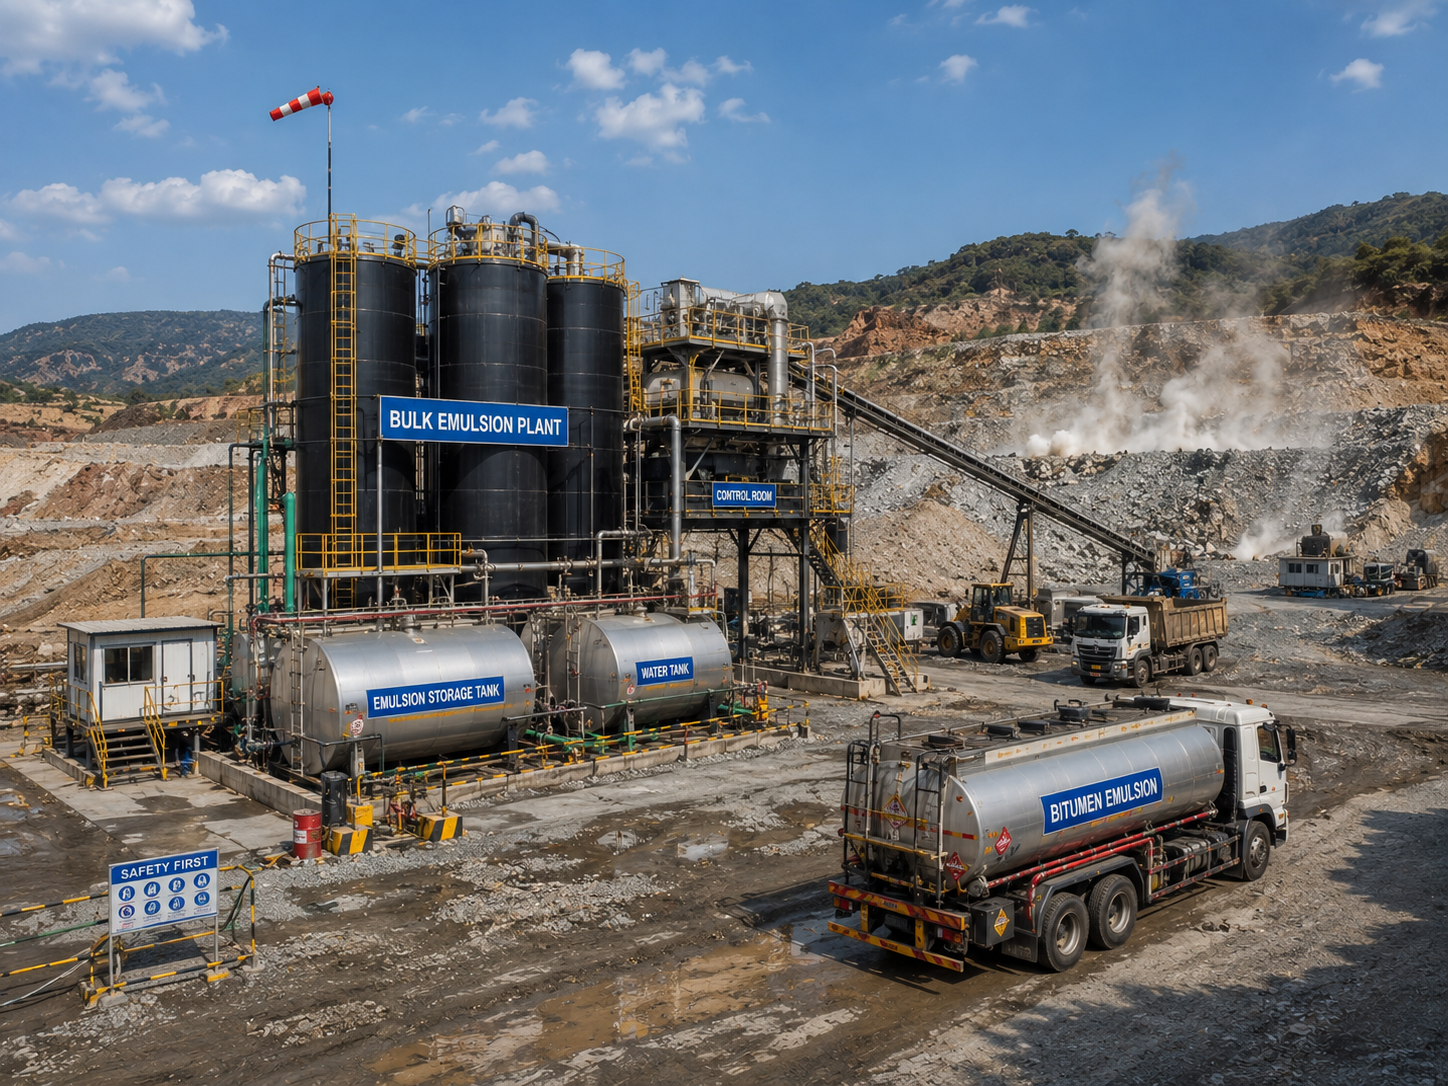
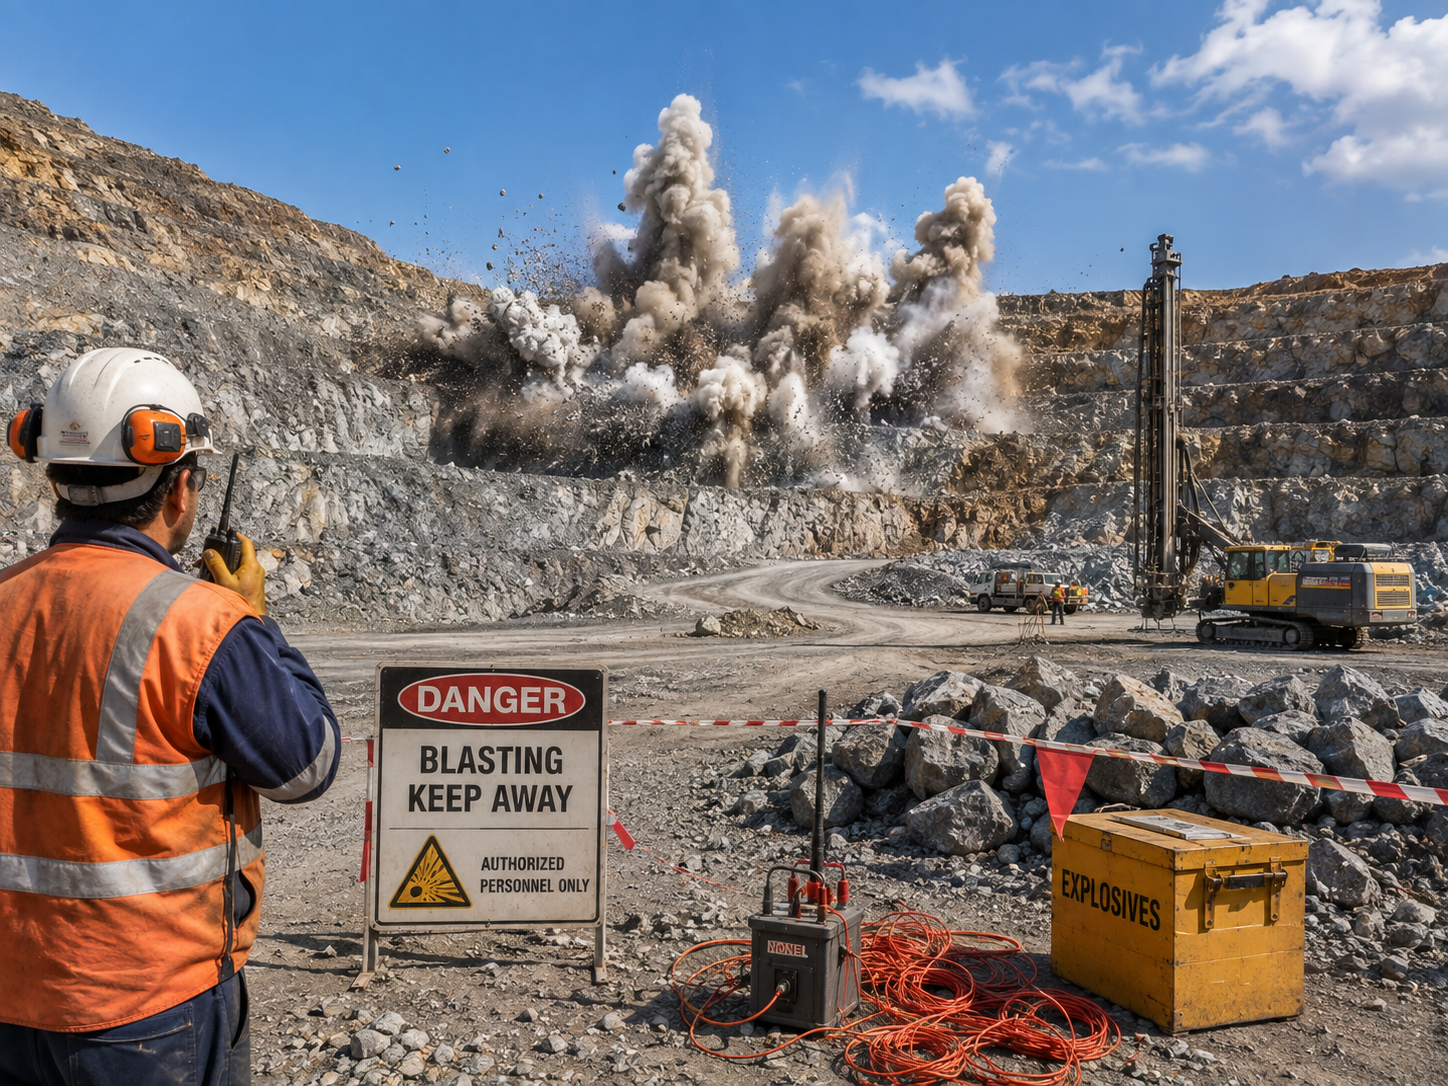
Explosives used for mining and construction blasting are typically manufactured and delivered as emulsions or gels — sensitive, shear-critical products that must be conveyed gently, safely and without pressure spikes. Any pump used in this process must operate reliably in a hazardous environment while protecting the stability of the product it handles.
The low-shear, virtually pulsation-free action of a progressive cavity pump makes it well suited to this duty. The rotor-stator design conveys product through sealed cavities rather than high-velocity impellers, minimising the risk of premature detonation-sensitising agitation and protecting the integrity of the emulsion.
The geometry is the safety case. There is no impeller, no high-velocity shear zone and no pulsation spike. Product is carried forward in sealed cavities at low speed — which is why this pump principle, rather than a centrifugal or piston alternative, suits shear-critical emulsions.
Three Reasons It Suits The Duty
Emulsion and gel explosives are unforgiving of the wrong pump. These are the properties that matter.
Sealed Cavity Conveying
Product is carried through sealed cavities formed between rotor and stator, rather than accelerated by an impeller — so it is moved, not beaten.
- No high-velocity impeller zone
- Low rotational speed
- Protects the integrity of the emulsion
No Pressure Spikes
Virtually pulsation-free delivery means flow arrives steady rather than in pulses, avoiding the pressure spikes that a shear-critical product cannot tolerate.
- Virtually pulsation-free flow
- Controlled, even delivery rate
- Minimises detonation-sensitising agitation
Hazardous Environment Duty
Any pump used in this process must operate reliably in a hazardous environment while protecting the stability of the product it handles.
- Reliable operation in hazardous areas
- Configured to site safety requirements
- Consistent performance across duty cycles
ROTOMAC Pumps For The Explosives Industry
Four duties from mixing vessel to blast site.
Emulsion Explosives Transfer
Our S Range pumps convey viscous explosive emulsions from mixing vessels to storage or bulk delivery trucks with low shear and controlled, pulsation-free flow.
Bulk Loading At Site
Our compact pump configurations support metered, on-demand loading of emulsion product into mobile mixing units for delivery directly to the blast site.
Raw Material Metering
Oxidiser solutions, fuel-oil phases and emulsifying agents are accurately metered using our MP & LA Dosing Range, supporting consistent product formulation and quality.
Site Wastewater And Wash-Down
Wash-down water and residues from mixing and loading areas are handled by our S Range and Open Hopper pumps for safe treatment and disposal.
Pump Ranges For Explosives
The ranges most often specified for this sector. Send us your duty and our engineers will confirm the model.
S Range
Robust all-round progressive cavity pumps conveying low to highly viscous products, with or without solids.
W Range
Open hopper pumps with integrated auger feed for highly viscous, semi-solid and non-flowable products.
Dosing Range
Precise metering of low to highly viscous, aggressive media with high accuracy and minimal pulsation.
Specifying A Pump For Emulsion Handling?
Tell us the product, the viscosity, the transfer rate and the area classification — our engineers will configure a pump suited to shear-critical duty in a hazardous environment.
Email Us
contact@rotomac.orgCall Us
+91 7522 002204 (Sales)Head Office
D-4a, Panki Industrial Area, Site-1, Kanpur – 208022, India